Winwon Chips
Choosing components for a bulk order is rarely as simple as comparing prices. A small sample can reveal problems that product photos and datasheets never show. Pin spacing may drift. Plating may look uneven under bright light. A connector can fit perfectly once, then fail after repeated insertion.
What is the best way to sample electronic components before bulk order? The answer is a controlled, evidence-based process that matches samples with real production conditions. Request samples from the exact manufacturer, factory, and revision intended for mass supply. Record part numbers, date codes, packaging details, and supplier statements. Keep every document together.
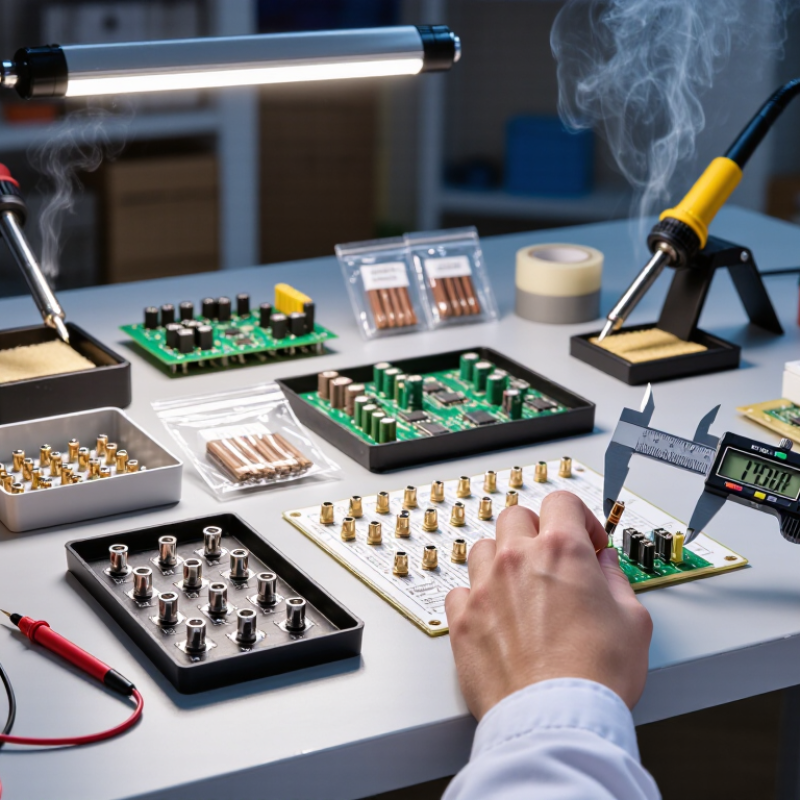
Test more than basic functionality. Check dimensions with calibrated tools. Measure electrical performance across normal and stress conditions. Inspect solderability, labeling, surface finish, and mechanical strength. If the component is used in a finished assembly, run a small pilot build. Five successful bench tests may still hide a process issue.
Ask direct questions.
Can the supplier reserve the same source? Will materials change without notice? How are rejected lots handled? Reliable suppliers should provide clear answers, traceable records, and consistent communication. Independent laboratory testing can add confidence for critical components, especially when failure would affect safety, warranty costs, or production schedules.
A practical sample plan should also define acceptance criteria before testing begins. Otherwise, teams may approve a sample because it “looks fine.” That judgment is convenient, but weak. I have seen promising samples pass early checks and disappoint during longer production runs. Sampling cannot remove every risk, yet it can expose expensive surprises while changes remain manageable.
2026 Best Way to Sample Components Before a Bulk Order?
Define Sampling Goals and Bulk Order Requirements
A reliable sample begins with a clear buying decision. Define the component’s function, tolerances, materials, finish, lifespan, and expected monthly volume. Record the conditions it must survive, such as vibration, heat, moisture, or repeated assembly. McKinsey reported that 93% of supply chain leaders planned to increase resilience after major disruptions. Your sampling plan should reflect that concern.
Do not test only appearance. Compare dimensions, performance, packaging, labeling, and inspection records against the bulk-order specification. Request samples from the intended production process, not a special workshop batch. Set measurable acceptance criteria before delivery. For example, permit a 0.2 mm dimensional deviation only when engineering confirms it is safe. This step is often skipped. It can become expensive later.
Tips: Order enough samples for testing, destructive checks, and independent review. Keep one sealed reference sample. Photograph defects beside a scale. Ask for material certificates and process-control data. A small pilot order may expose handling problems that five perfect samples hide. The 2022 ASQ Quality 4.0 research emphasizes data-driven quality decisions, but data still needs context. I would challenge one common assumption: a passed sample does not guarantee stable bulk production. Recheck critical features during the first production run.
| Component Category | Primary Sampling Goal | Recommended Pre-Order Sample Quantity | Checks and Tests Before Approval | Typical Acceptance Criteria | Bulk Order Requirements to Define | Recommended Sampling Approach |
|---|---|---|---|---|---|---|
| Electronic ICs and Semiconductor Devices | Confirm electrical performance, package quality, traceability, and compatibility with the intended circuit. | 10–30 pieces Use at least 3 production lots when lot-to-lot variation is a concern. |
Visual inspection, package and marking verification, pin and lead inspection, dimensional checks, functional test, temperature or voltage margin test, and solderability review. | All samples meet the approved datasheet limits at the specified operating conditions; no counterfeit, damaged, remarked, or mixed-lot parts. | Exact part revision, approved manufacturer or source restrictions, date-code limits, moisture-sensitive-device handling, packaging format, certificates of conformity, and traceability records. | Test samples from more than one lot. Require a first-article approval before releasing the full purchase order. |
| Passive Components Resistors, capacitors, inductors |
Verify value, tolerance, voltage or power rating, physical size, and stability under operating conditions. | 20–50 pieces Include samples from the minimum and maximum expected values. |
Value measurement, tolerance verification, insulation resistance, dielectric withstand where applicable, temperature coefficient, ESR or impedance where relevant, and dimensional inspection. | Measured values remain within the stated tolerance; no cracks, lifted terminations, damaged coatings, or out-of-specification dimensions. | Resistance or capacitance value, tolerance, rated voltage, temperature range, package size, material or dielectric type, reel quantity, label format, and storage conditions. | Use a small engineering sample first, then repeat testing on production-intent samples before approving the bulk lot. |
| Connectors and Switches | Confirm mating compatibility, contact reliability, mechanical fit, and resistance to repeated use. | 15–30 pieces Include mating parts and cable assemblies when applicable. |
Dimensional inspection, mating and unmating force, contact resistance, retention force, continuity, insulation resistance, dielectric withstand, and insertion-cycle testing. | All samples fit the approved interface; contact resistance remains stable; no cracked housings, loose terminals, intermittent continuity, or excessive mating force. | Number of positions, pitch, plating specification, terminal material, current and voltage ratings, keying, locking method, mating-cycle target, packaging, and inspection level. | Test the complete mating system rather than the individual connector only. Use production tooling and the intended cable or PCB during validation. |
| Wires and Cable Assemblies | Verify conductor size, insulation quality, pinout, termination strength, and electrical safety. | 10–20 assemblies For complex harnesses, sample each unique configuration. |
Conductor resistance, continuity, insulation resistance, dielectric withstand, crimp pull force, terminal retention, bend test, length and labeling inspection. | Correct pinout and length; no open or short circuits; insulation and dielectric results meet the approved specification; terminations withstand the defined pull force. | Conductor cross-section, insulation material, temperature rating, voltage rating, cable length, connector orientation, wire color, labeling, bend radius, and test records. | Approve a golden sample and a wiring drawing. Require 100% continuity testing for every production assembly when miswiring could create a safety risk. |
| Printed Circuit Boards | Validate stack-up, dimensions, hole quality, surface finish, solderability, and fabrication capability. | 5–10 bare boards Use 3–5 assembled boards for functional validation. |
Layer count and stack-up review, dimensional and hole inspection, copper thickness verification, solderability, microsection analysis where required, electrical test, and assembly fit check. | No shorts or opens; dimensions and tolerances match the approved drawing; plating and solder mask are intact; boards pass electrical and functional tests. | Material type, layer count, finished copper thickness, surface finish, minimum trace and space, impedance targets, board thickness, panelization, fabrication class, and test method. | Use first-article inspection on production panels. Confirm the approved data package, revision level, and controlled change process before bulk release. |
| Mechanical Fasteners Screws, nuts, washers, inserts |
Confirm dimensions, material, surface treatment, thread fit, torque behavior, and corrosion resistance. | 30–50 pieces Increase the sample for safety-critical or high-strength applications. |
Dimensional and thread-gauge inspection, hardness, tensile or proof-load testing, torque testing, coating thickness, visual inspection, and corrosion testing where required. | Thread gauges pass; dimensions and hardness meet the drawing; no damaged threads, burrs, plating defects, or premature coating failure. | Thread standard and size, material grade, strength class, head style, coating, corrosion requirement, torque range, lot definition, packaging, and cleanliness limits. | Verify samples using calibrated gauges and test equipment. Keep samples from each material or coating lot when performance is critical. |
| Molded Plastic Parts Housings, covers, brackets |
Confirm fit, appearance, dimensions, material, strength, and consistency of the molding process. | 10–20 pieces Include parts from different cavities when multi-cavity tooling is used. |
Dimensional measurement, assembly fit, visual inspection, material verification, warpage measurement, color comparison, impact or load testing, and environmental exposure where relevant. | All critical dimensions meet drawing tolerances; parts assemble without excessive force; no sink marks, flash, cracks, short shots, or unacceptable warpage. | Resin grade, flame rating, color standard, surface texture, shrinkage allowance, critical dimensions, mold cavity identification, allowable regrind, and cosmetic limits. | Approve a boundary sample showing acceptable and unacceptable cosmetic conditions. Inspect parts from every cavity during first-article production. |
| Rubber Seals and Gaskets | Verify sealing performance, material compatibility, compression behavior, and resistance to the intended environment. | 20–30 pieces Use samples from multiple production lots for critical sealing applications. |
Dimensional inspection, hardness, compression set, tensile or elongation testing, leak testing, fluid compatibility, temperature exposure, and visual inspection. | No leakage under defined pressure; dimensions and hardness meet the specification; no cracks, cuts, flash, tackiness, or permanent deformation beyond the limit. | Elastomer type, hardness, operating temperature, media compatibility, compression ratio, surface finish, storage life, packaging, cleanliness, and shelf-life requirements. | Test the seal in the actual mating hardware. Define storage and aging requirements before placing a long-lead-time bulk order. |
| Rechargeable Battery Packs | Confirm capacity, voltage, protection functions, safety, cycle performance, and transport documentation. | 10–20 packs Use a qualified laboratory for safety-critical testing. |
Capacity and energy measurement, charge and discharge testing, protection-circuit verification, temperature monitoring, dimensional inspection, cycle testing, and documentation review. | Capacity and voltage meet the approved specification; protection functions operate correctly; no swelling, leakage, overheating, or abnormal behavior. | Cell configuration, nominal voltage, capacity, chemistry, protection limits, connector, enclosure, cycle-life target, UN 38.3 documentation, safety data, and transport classification. | Do not rely on appearance-only sampling. Complete electrical and safety validation before approving production quantities or shipment. |
Define the function, dimensions, tolerances, materials, finish, lifespan, and monthly volume. Record exposure to heat, moisture, vibration, and repeated assembly.
Order enough for performance tests, destructive checks, and independent review. Keep one sealed reference sample. Five perfect pieces may hide process variation.
Yes. Request samples made through the intended production process, not a special workshop batch. This better reflects likely bulk-order consistency.
Set measurable limits before delivery. A 0.2 mm deviation might be acceptable, but engineering must confirm its safety. This step is easy to skip.
Request material certificates, inspection records, and process-control data. Photograph defects beside a ruler or scale. Keep measurements with each sample.
Include the sample price, tooling, shipping, taxes, inspection, and possible rework. A low unit price can hide expensive setup charges. I once missed inspection costs.
Record production, inspection, and dispatch times separately. Compare promised dates with actual delivery. Fast replies do not guarantee reliable schedules.
Inspect bags, moisture protection, labels, carton strength, and internal separators. Photograph crushed corners and loose parts immediately. Small packaging flaws matter.
Ask who handles technical questions, drawing changes, defects, and replacements. Look for replies containing measurements and dates. Vague answers need caution.
No. Recheck critical features during the first production run. A passed sample is evidence, not proof. This assumption deserves another look.
What is the best way to sample electronic components before bulk order? Start by defining clear sampling goals and documenting the requirements for the planned purchase, including specifications, quantities, operating conditions, certifications, packaging, and delivery expectations. Then identify qualified suppliers and request representative samples from the same production source intended for the bulk order. This helps ensure that the samples accurately reflect future manufacturing quality rather than being specially prepared items.
Evaluate each sample for dimensions, materials, electrical or mechanical performance, compliance documentation, workmanship, and consistency across multiple units. Compare suppliers not only by unit price, but also by lead time, packaging protection, communication, technical support, and ability to maintain stable quality. After selecting the strongest sample, approve it against written acceptance criteria and establish pre-order controls such as inspection plans, traceability requirements, change-notification procedures, and batch testing. This structured process reduces quality risks, improves purchasing decisions, and creates a clear quality standard before production begins.